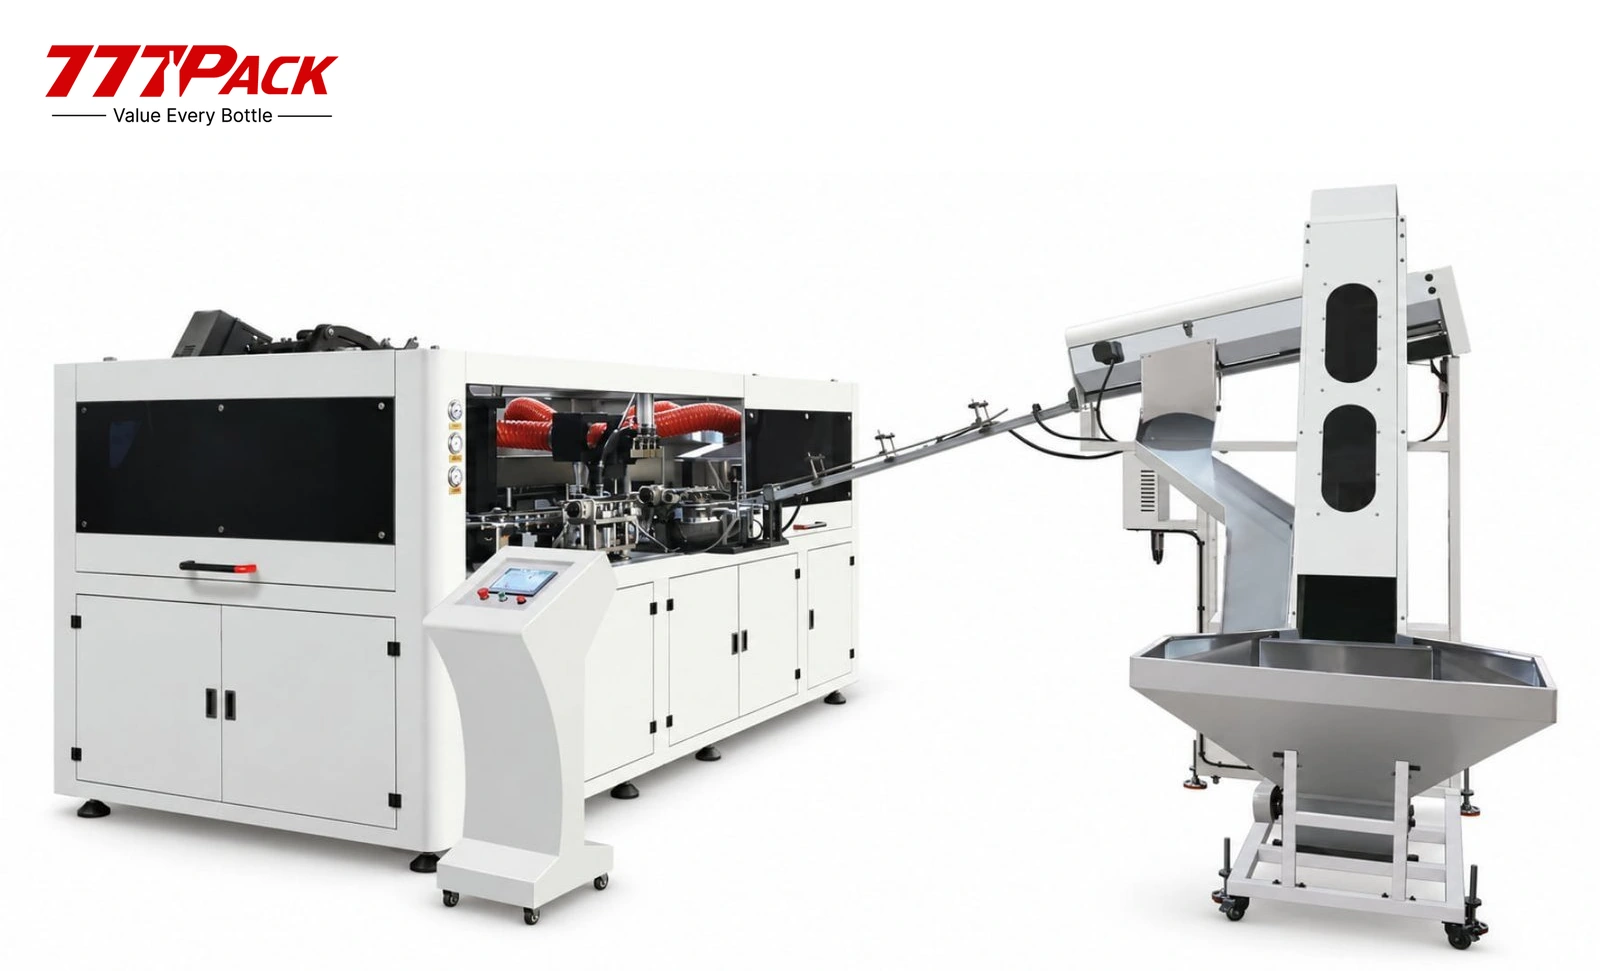
Full Servo High-Speed Automatic PET Bottle Blowing Machine
Model:LGG Series
Automatic PET stretch blow molding with servo-driven mold clamping, stretching and transfer. Five LGG models cover theoretical output of 5,500–13,000 BPH and maximum bottle volumes of 0.75L or 1.5L.
Line integration
Position in the Production Line
The current stage is highlighted. This example shows how the equipment connects within the selected line.
- Parallel preparation01AWater TreatmentFilter · Purify · Disinfect01BBottle BlowingPreform to BottleCURRENT
- 02FillingRinse · Fill · Cap
- 03DryingRemove Surface Moisture
- 04CodingDate · Batch · Traceability
- 05LabelingSleeve · Hot Melt · Self-Adhesive
- 06PackingFilm · Carton · Tray
- 07PalletizingStack Finished Packs
Swipe or scroll to explore all stages →
Reference flow only. Final process and equipment scope depend on the product, container, output and project requirements. Each stage links to its equipment or equipment category.
Equipment Overview
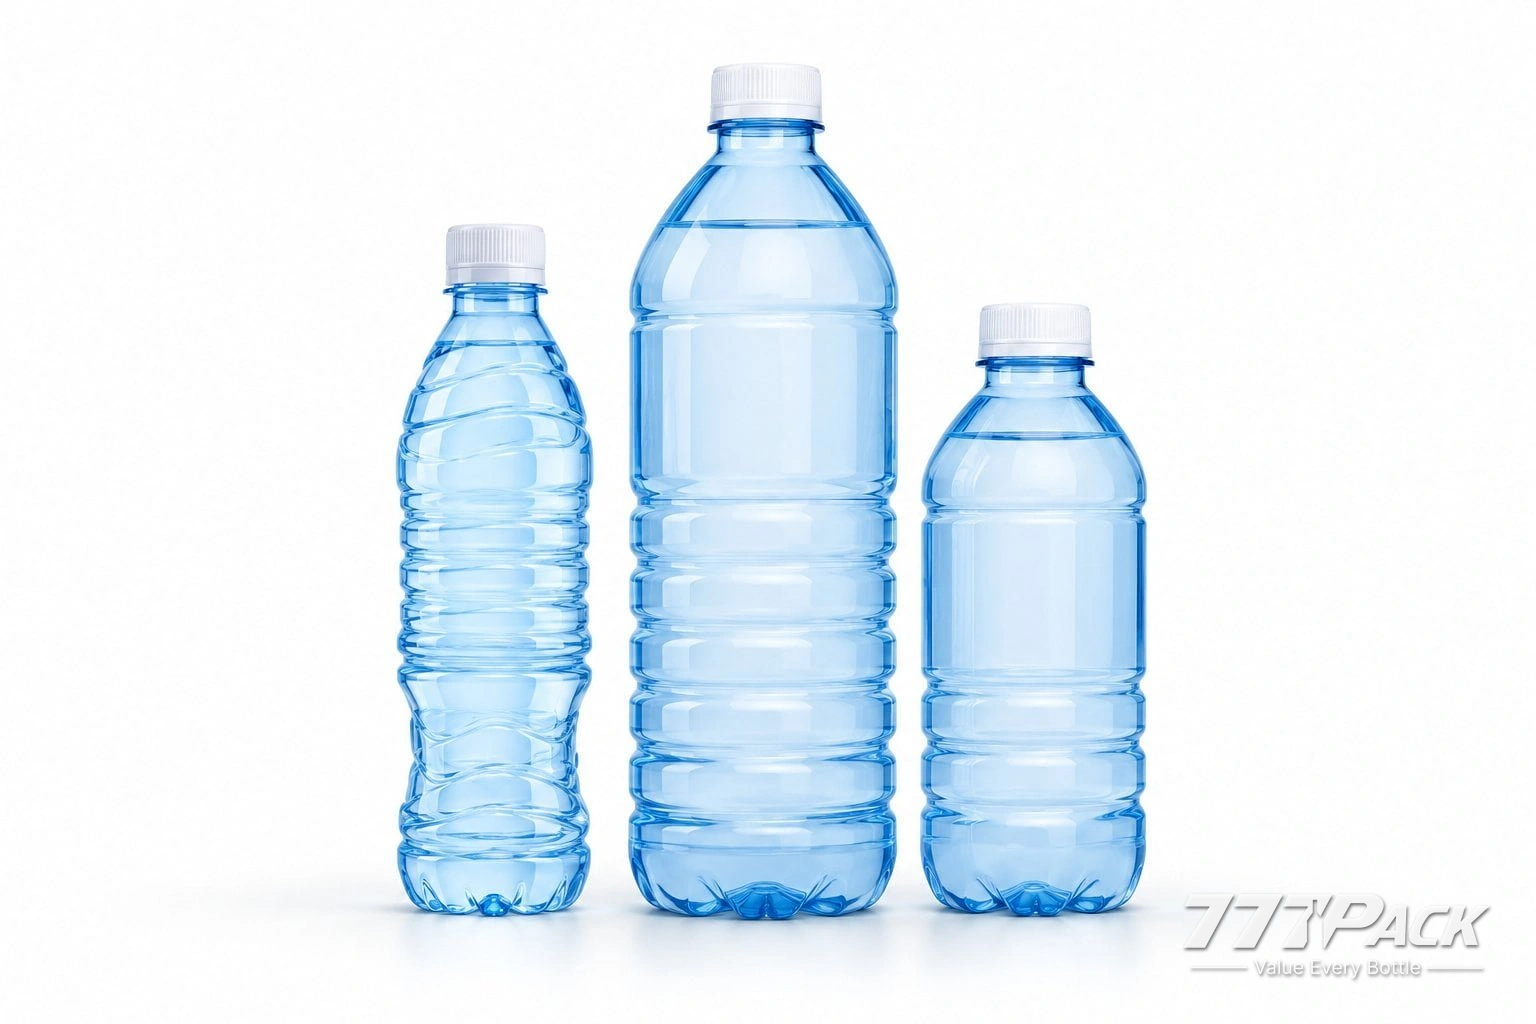
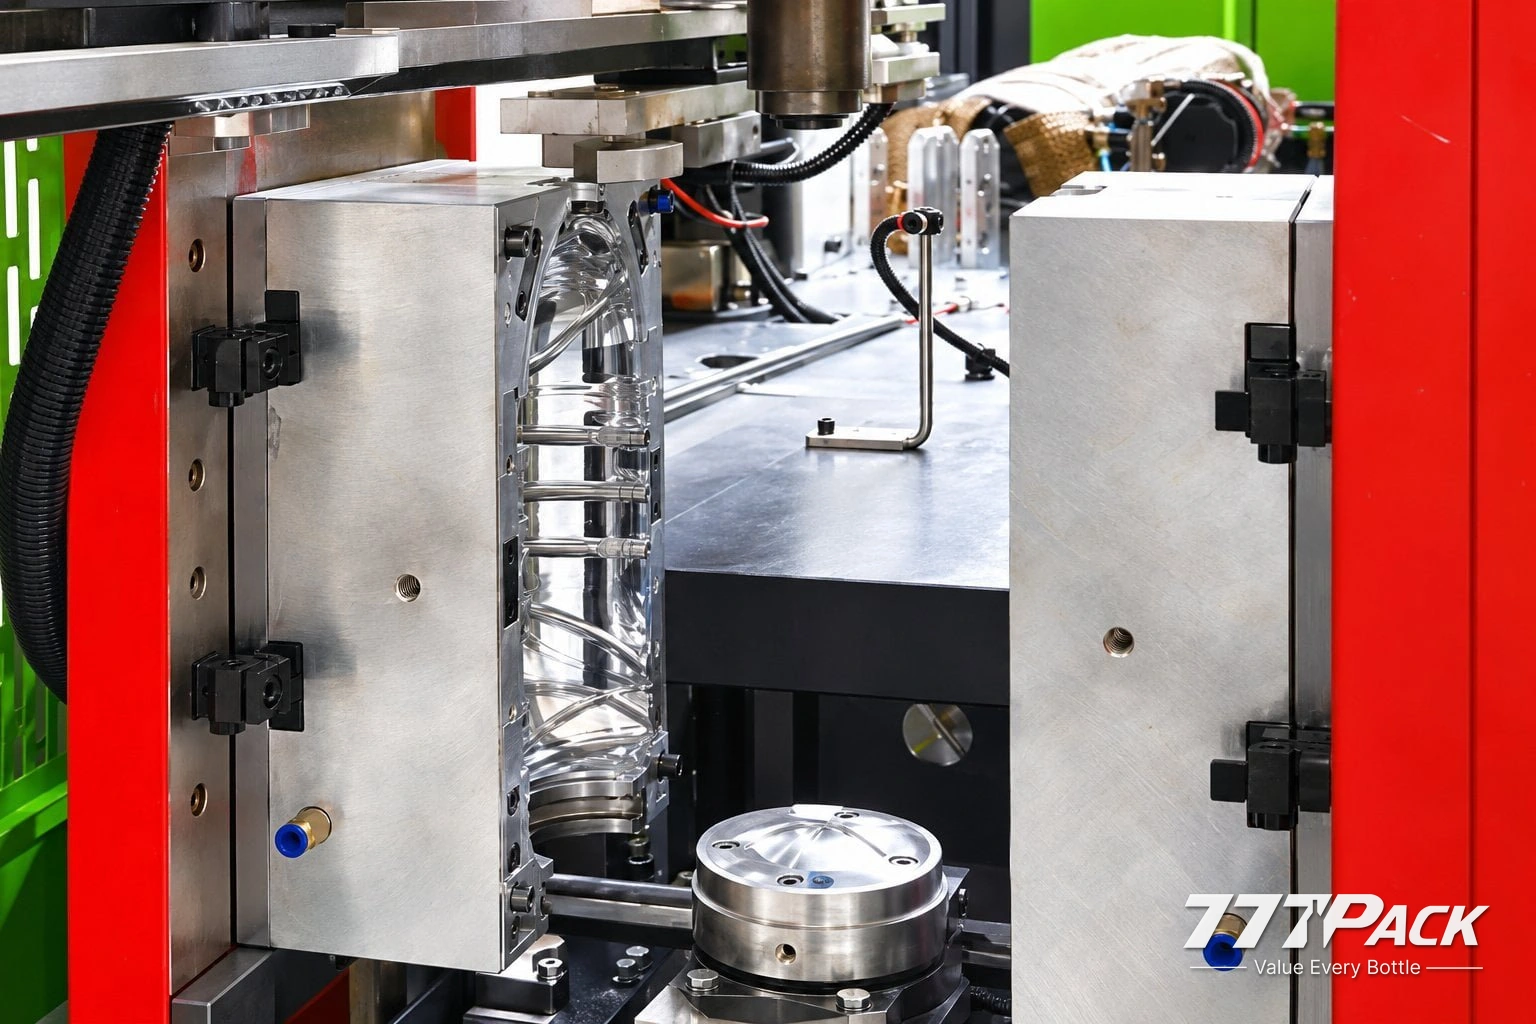
The LGG Series Full Servo High-Speed Automatic PET Bottle Blowing Machine converts PET preforms into bottles for water production. Servo-driven clamping, stretching and transfer coordinate the forming cycle across 4-, 6- and 9-cavity configurations.
Choose the model against bottle volume, diameter, height, neck dimensions and required output. Maximum bottle volume is 0.75L or 1.5L by model; final output is confirmed with the approved preform and bottle design.
Machine Details
Full Servo High-Speed Automatic PET Bottle Blowing Machine
Full Servo High-Speed Automatic PET Bottle Blowing Machine
Core Specifications
| Mold Thickness — All Models | 210 mm |
|---|---|
| Mold Stroke — LGG-4-750 / 4-15 / 6-750 / 6-15 / 9-750 | 100 / 130 / 100 / 130 / 100 mm |
| Stretching Stroke — Same Model Order | 76.2 / 100 / 76.2 / 100 / 76.2 mm |
| Preform Elevator — 4- and 6-Cavity Models | 1,960 × 1,460 × 2,550 mm |
| Preform Elevator — LGG-9-750 | 2,560 × 1,460 × 2,550 mm |
| Working Air Pressure | 0.8 MPa |
| Blowing Air Pressure | ≤3.5 MPa |
Model Comparison
LGG Full-Servo PET Bottle Blowing Machine Models
Five LGG configurations. Output is theoretical and depends on the confirmed preform, bottle and operating conditions.
| Model | Theoretical Output | Cavities / Max. Volume | Max. Bottle Size (Neck / Ø / H) | Installed / Reference Running Power | Main Machine (L × W × H) / Weight |
|---|---|---|---|---|---|
| LGG-4-750 | 6,500–7,000 BPH | 4 cavities · 0.75L max. | 45 / 69 / 260 mm | 58 / 20–25 kW | 3,900 × 2,100 × 2,100 mm · 5,000 kg |
| LGG-4-15 | 5,500–6,000 BPH | 4 cavities · 1.5L max. | 45 / 93 / 330 mm | 58 / 30–35 kW | 4,500 × 2,100 × 2,100 mm · 5,500 kg |
| LGG-6-750 | 8,500–9,000 BPH | 6 cavities · 0.75L max. | 45 / 69 / 260 mm | 58 / 35–40 kW | 4,600 × 2,100 × 2,100 mm · 6,000 kg |
| LGG-6-15 | 7,000–7,500 BPH | 6 cavities · 1.5L max. | 45 / 93 / 330 mm | 96 / 45–50 kW | 6,200 × 2,100 × 2,100 mm · 6,600 kg |
| LGG-9-750 | 13,000 BPH | 9 cavities · 0.75L max. | 45 / 69 / 230 mm | 96 / 45–50 kW | 6,500 × 2,000 × 2,100 mm · 7,500 kg |
Note. Output follows the supplied model table; stable production speed is confirmed with the approved bottle and preform. Reference running power varies with operating conditions. Specifications are subject to final technical confirmation.
Working Principle
Engineering Highlights
Practical design details that affect operation, changeover, hygiene and maintenance.
Servo-Driven Forming
Full-Servo MotionsClamping, stretching and transfer are driven by servo motors.
Model-Matched Output
4 · 6 · 9 CavitiesChoose cavity count and bottle-volume limits against the line demand.
Positioned Mold Installation
Positioned mold installation supports repeatable setup during bottle changes.
Line Integration
Line Integration
Equipment role and interfaces for this reference application.
Forms empty PET water bottles from heated preforms while water treatment runs in parallel. Finished bottles transfer to rinsing, filling and capping, followed by drying, coding, labeling, packing and palletizing.
- Preform Supply: Approved PET preforms matched to neck finish, weight and bottle design.
- Bottle Discharge: Transfer and conveying matched to the downstream rinser-filler-capper.
- Line Controls: Coordinate bottle output, buffer capacity and upstream/downstream signals.
Standard and Optional Configuration
- Full-Servo Forming Motions
Servo-driven mold clamping, stretching and transfer.
- Automatic Preform Feeding
Preform elevator and transfer system feed the heating and blowing cycle.
- Bottle Heating & Forming
Heating and stretch-blowing setup matched to the confirmed preform and bottle.
- Additional Bottle Molds
Extra approved bottle shapes and sizes within the selected model limits.
- Compressed-Air & Cooling Package
Air treatment, storage and cooling equipment sized for the project.
Utilities and Installation
Working Air
0.8 MPa; clean, dry air; flow confirmed by model.
Blowing Air
Up to 3.5 MPa as specified; pressure and air consumption confirmed with bottle samples.
Electrical Supply
58 or 96 kW installed power by model; voltage and frequency confirmed for the destination.
Cooling
Cooling-water temperature and flow confirmed against mold and production rate.
Installation
Allow space for the main machine, elevator, hopper, utilities and maintenance access.
Before You Decide
Frequently Asked Questions
Answers to common questions about selection, integration and project planning.
What bottle sizes can the LGG PET bottle blowing machine produce?
Maximum volume is 0.75L or 1.5L by model. Bottle diameter, height, neck finish and preform design must meet the selected model’s limits.
Is the stated output guaranteed for every bottle?
No. The supplied figures are theoretical output. Stable speed is confirmed with the actual preform, bottle weight, heating recipe, cooling and air supply.
How does the machine connect to a PET water filling line?
Bottle blowing runs in parallel with water treatment. Empty bottles transfer to rinsing, filling and capping, followed by drying, coding, labeling, packing and palletizing.
Line Solutions
Compatible Production Lines
Explore related equipment, line solutions and delivered projects.
Project Evidence
Related Projects
Explore related equipment, line solutions and delivered projects.
Project Services
Manufacturing & Line Integration
Core equipment manufacturing, auxiliary-machine coordination and complete-line integration are managed as one system to reduce interface risks before delivery.
FAT & Quality Inspection
Project checks before packing and delivery.
Installation & Commissioning
On-site setup, testing and operator training.
Local Support in Indonesia
Local coordination for service and spare parts.
Let us match the right equipment solution.
Send these four project details. We will recommend the technology, output configuration and line connection plan.